Table of Contents
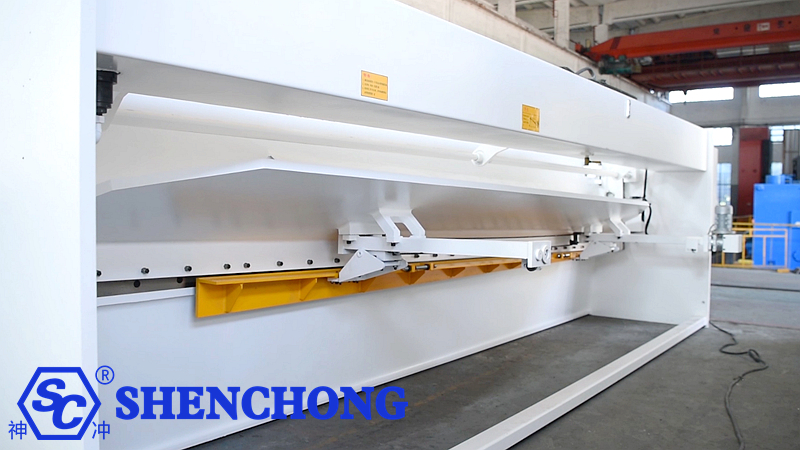
Improving the precision of hydraulic guillotine shearing requires more than just adjusting the backgauge. Precision is determined by the combined interaction of the mechanical structure, blade clearance, backgauge, hydraulic system, sheet positioning, frame rigidity, control system, and operational maintenance.
The following is a systematic analysis from a practical production perspective.
1. How to improve the precision of hydraulic guillotine shearing?
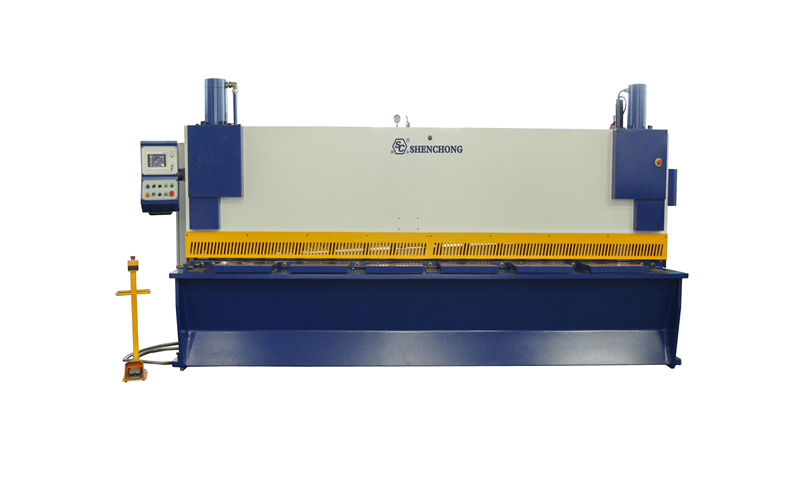
First, identify the core factors affecting guillotine shearing precision.
The final precision of a hydraulic guillotine shear is typically reflected in:
- Shear length precision
- Diagonal precision
- Straightness
- Squareness (perpendicularity)
- Shear edge quality
- Repeat positioning precision
- Consistency in batch processing
This can be summarized as:
Shearing Precision = Frame Rigidity + Blade Condition + Blade Clearance Control + Backgauge Precision + Hydraulic Stability + Positioning Method + Correct Operation
Significant errors in any of these areas can result in final dimensions falling outside tolerance limits.
2. 15 Key Aspects for Improving Precision
1) Enhancing the rigidity of the hydraulic guillotine shearing machine frame and blade carrier
This is the fundamental requirement.
When a hydraulic guillotine shear operates, the upper blade carrier is subjected to significant shearing forces. If the rigidity of the frame, worktable, or blade carrier is insufficient, minute deformations occur during the shearing of thick plates.
For example:
Shearing thin plates: Frame deformation has a relatively minor impact.
Shearing 10–20 mm thick plates: Shearing force increases significantly.
Insufficient frame rigidity can lead to:
- Inconsistent dimensions at the ends of the plate
- Deviation of the shear line
- Slight bending of the plate
- Increased diagonal error
- Inconsistent shear cross-section
- Improvement methods
Focus on inspecting:
- Frame weld quality
- Overall frame rigidity
- Upper blade carrier rigidity
- Worktable flatness
- Blade carrier guide clearance
- Wear on the guiding mechanism
- Synchronization between the left and right sides
For equipment designed to shear thick plates, a highly rigid frame combined with a sound structural design is more important than simply increasing hydraulic pressure.
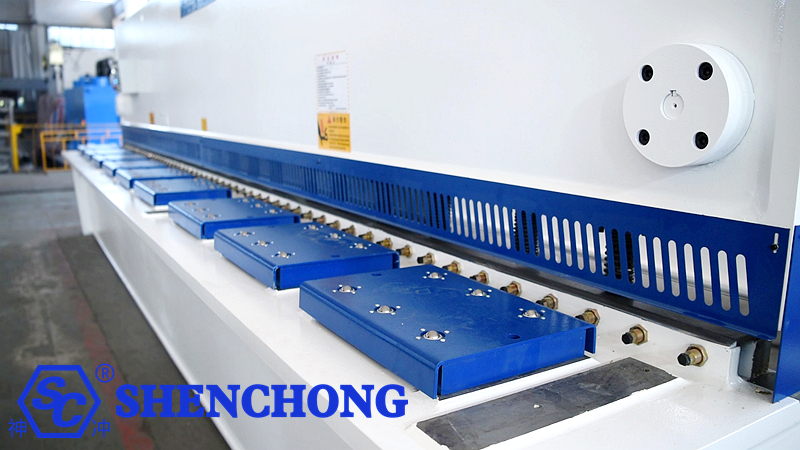
2) Precise control of blade clearance
This is one of the most critical factors affecting shear quality.
Excessive or insufficient blade clearance can both cause problems.
Excessive clearance tends to result in:
- Increased burrs
- Plate deformation
- Rough shear cross-section
- Edge rollover (collapse)
- Reduced dimensional stability
Insufficient clearance may cause:
- Increased shearing force
- Accelerated blade wear
- Blade edge chipping
- Increased hydraulic system load
- Abnormal crushing of the plate edge
Therefore, blade clearance must be adjusted based on plate thickness, material type, and material strength.
Typical approach:
Materials | Plate thickness | Blade clearance adjustment |
Ordinary carbon steel | Thin plate | Small |
Ordinary carbon steel | Medium-thick plate | Medium |
High-strength steel | Same thickness | Usually requires a more appropriate/larger clearance |
Stainless steel | Same thickness | Adjust appropriately based on material strength |
Aluminum sheet | Thin plate | Usually employs a small, stable clearance |
Do not use a fixed blade clearance to process all materials.
3) Improving the accuracy of the backgauge system
For CNC hydraulic guillotine shears, the backgauge system is a key component determining the accuracy of the cutting length.
The backgauge primarily controls the distance from the cutting edge to the positioning point.
For example, if a cut length of 2500 mm is required, but the actual backgauge position is only 2498.5 mm, a dimensional error in the workpiece will inevitably occur.
Key components of the backgauge to inspect include:
- Lead screw
- Guide rails
- Servo motor
- Reduction mechanism
- Encoder
- Backgauge fingers
- Beam rigidity
- Mechanical clearance
- Backlash
4) High backgauge repeatability
If:
First piece: 500.00 mm
Second piece: 500.05 mm
Third piece: 499.98 mm
This type of discrepancy is classified as a repeatability error.
This is particularly critical for batch production.
Recommended components:
- High-precision servo motor
- High-precision ball screw
- Linear guide rails
- High-resolution encoder
- Rigid backgauge beam
Additionally, perform regular repeatability tests.
For example, 10 consecutive positioning cycles:
Count | Actual measurements |
1 | 500.02 |
2 | 500.01 |
3 | 500.03 |
4 | 500.00 |
5 | 500.02 |
6 | 500.01 |
7 | 500.02 |
8 | 500.04 |
9 | 500.01 |
10 | 500.02 |
By analyzing the maximum, minimum, and average values, the actual repeatability of the backgauge system can be determined.
5) Ensure the sheet is properly seated against the backgauge
This is an issue often overlooked in actual production environments.
Even if the machine itself has high precision, errors will occur if the sheet is not fully flush against the backgauge.
If the sheet is tilted, the final cut dimensions will be inaccurate.
Key operational steps
Before shearing:
- Place the sheet on the worktable.
- Align the sheet edge against the positioning device.
- Ensure the sheet is parallel to the backgauge.
- Eliminate any gap between the sheet and the backgauge.
- Initiate the shearing process.
For large sheets, consider using:
- Front supports
- Pneumatic sheet lifters
- Sheet support arms
- Front feeding systems
- Automatic loading systems
These help minimize positional errors caused by manual handling.
6) Ensure stable hydraulic system pressure
The hydraulic system itself affects shearing stability.
Unstable hydraulic pressure can lead to:
- Fluctuations in shearing speed
- Unstable movement of the upper blade carrier
- Lack of synchronization between left and right sides
- Vibration during shearing
- Difficulty shearing thick plates
- Reduced repeatability
Key components to check:
- Hydraulic pump
- Proportional valve
- Relief valve
- Solenoid valve
- Hydraulic cylinder
- Seals
- Hydraulic oil
- Oil temperature
- Oil cleanliness
Pay special attention to:
Hydraulic oil contamination is a significant hidden cause of precision loss in hydraulic shears.
High levels of contaminants in the hydraulic oil can cause unstable valve spool movement, which in turn affects the movement of the blade carrier.
7) Control synchronization of left and right cylinders
Swing-beam or guillotine shears typically drive the blade carrier using left and right hydraulic cylinders.
If the position of the left cylinder does not match that of the right cylinder:
The blade carrier may tilt.
This directly affects:
- Blade clearance
- Shearing angle
- Shearing quality
- Sheet deformation
- Dimensional consistency across the width
Therefore, the synchronization of the left and right cylinders and the levelness of the blade carrier must be checked regularly.
8) Control the shearing angle
The shearing angle also affects precision.
Excessive shear angle:
- Reduced shear force
- Potential increase in sheet deformation
- Changes in the sheared edge profile
Insufficient shear angle:
- Increased shear force
- Increased load on the hydraulic system
- Higher energy consumption
Therefore, the appropriate shear angle should be selected based on the plate thickness and material.
For CNC guillotine shearing machine, proper control of the shear angle allows for a balance between shear force, sheet deformation, and shear quality.
9) Blades must be kept sharp
Blade condition directly affects shearing precision.
Blade wear leads to:
- Increased burrs
- Sheet deformation
- Rough cut edges
- Reduced dimensional stability
- Increased shearing force
Wear is particularly rapid when processing:
- Stainless steel
- High-strength steel
- Thick steel plate
- Nickel plate
- High-hardness materials
It is recommended to establish a blade management system.
Keep records of:
Cumulative cutting length → Blade wear → Number of blade rotations/flips → Replacement schedule
Also, pay attention to the following after blade installation:
- Parallelism
- Height consistency
- Tightness of mounting bolts
10) Select appropriate blade materials
Different materials require different blades.
Common blade materials include:
9CrSi
6CrW2Si
Cr12MoV
H13
High-performance alloy tool steels, etc.
For example, the requirements for blade wear resistance and toughness differ between ordinary low-carbon steel and high-strength stainless steel.
If the blade choice is unsuitable, even a high-precision machine may experience:
Rapid blade wear → Changes in blade clearance → Increased burrs → Reduced dimensional stability
11) Improve worktable flatness
The worktable serves as the foundation for sheet positioning.
Issues such as:
- Localized depressions
- Welding deformation
- Wear
- Foreign objects
- Burrs
…prevent the sheet from lying flat and stable.
The impact is particularly significant for thin sheets and large-sized plates.
Therefore, the worktable must be kept:
Clean + Flat + Free from significant deformation.
12) Use front support and rear sheet-supporting devices
For large-sized plates such as:
4×2000 mm, 6×3200 mm, 8×4000 mm, 12×4000 mm, 16×6000 mm
…relying solely on the operator to hold the sheet often leads to tilting.
Consider using:
- Front support arms: To reduce errors caused by manual support.
- Pneumatic sheet support: Suitable for thin sheets and large-sized plates. Automatic front feeding: Further reduces errors caused by manual positioning.
- For large-scale shearing machines:Automatic feeding + rear support + front support
These features can significantly improve consistency in mass production.
13) Selecting the correct shearing speed
Many people believe:
The faster the cut, the higher the productivity.
However, for certain materials and thicknesses, an excessively fast shearing process can exacerbate issues such as sheet deformation and vibration.
Therefore, the speed should be selected based on:
- Plate thickness
- Material type
- Shearing length
- Shearing angle
- Blade clearance
For precision machining, stability is often more important than simply pursuing maximum speed.
14) Avoid shearing beyond specifications
This is a crucial point.
For example, if a machine is rated at 12 × 3200 mm:
This indicates the maximum shearing capacity for a specified range of material strengths.
If the equipment is consistently used to shear:
- Overly thick plates
- High-strength steel
- Stainless steel
- High-hardness materials
It may lead to:
Hydraulic system overload + blade wear + frame deformation + blade carrier issues + reduced accuracy
Therefore, one should not simply assume: “If the machine can cut through it, it is safe to do so long-term.”
Operations should be matched to the equipment’s rated parameters and the material’s strength.
15) Establish an "accuracy inspection and calibration" system
This is one of the most effective ways to maintain long-term accuracy.
Regular inspections are recommended for:
① Backgauge positioning accuracy
For example:
100 mm
500 mm
1000 mm
2000 mm
3000 mm
Measure each position individually.
② Diagonal measurements
For rectangular workpieces: compare the two diagonals.
If the difference is significant, it indicates issues with positioning or the orientation of the sheet.
③ Straightness
Check the sheared edge for:
- Bulging in the middle
- Offset at the ends
- Localized bending
④ Repeatability of positioning
Perform positioning tests 10 or more times consecutively.
3. Troubleshooting directions corresponding to different errors
This is a very practical chart for the production floor.
Issue | Primary Causes | Priority Checks |
Overall length consistently too long | Incorrect backgauge position | Backgauge Calibration |
Overall length consistently too short | Incorrect backgauge position | Parameter Compensation |
First piece accurate, but subsequent pieces show increasing deviation | Thermal drift / Mechanical backlash | Backgauge, Servo |
Inconsistent dimensions between left and right sides | Sheet misalignment / Shear beam issues | Positioning, Ram/Blade Holder |
Significant diagonal error | Non-perpendicular positioning | Backgauge, Side Positioning |
Excessive burrs | Improper blade clearance / Blade wear | Blade Clearance, Blades |
Excessive burrs on one side | Uneven blade clearance (left vs. right) | Blade Installation |
Sheet distortion | Blade clearance / Shear angle / Material issues | Blade Clearance, Angle |
Rough sheared edge | Blade wear | Replacement/Blade Reversal |
Difficulty shearing thick plates | Insufficient pressure / Exceeding specifications | Hydraulic System |
Unstable repeat positioning | Lead screw or guideway backlash | Backgauge |
Left and right blade carriers out of sync | Hydraulic synchronization issues | Cylinder, Valve Block |
4. Key areas for improving precision based on material thickness
1-3 mm thin sheets
Key focus:
Backgauge precision + Sheet flatness + Blade clearance
Thin sheets are particularly susceptible to warping.
4-8 mm medium plates
Key focus:
Blade clearance + Backgauge + Blade sharpness + Frame rigidity
10-16 mm thick plates
Key focus:
Frame rigidity + Hydraulic system + Blades + Blade clearance + Shear angle
Plates thicker than 20 mm
Shift in focus:
Equipment rated capacity + Frame deformation + Hydraulic stability + Blade strength + Material strength
Do not focus solely on the backgauge.
5. Higher automation precision
Modern CNC hydraulic guillotine shearing lines can be further equipped with:
CNC control system
↓
Servo backgauge
↓
Automatic blade clearance adjustment
↓
Front feeding system
↓
Automatic sheet support
↓
Sheet detection
↓
Automatic shearing
↓
Automatic material unloading
This transforms “manual, experience-based shearing”
into “digitized, automated, and repeatable precision shearing.”
6. Top 5 priorities for improvement
If an existing hydraulic guillotine shearing is underperforming in terms of precision, I recommend troubleshooting in the following order rather than replacing all components at once:
First: Backgauge
Check actual position and repeatability.
Second: Blade clearance
Recalibrate based on material type and thickness.
Third: Blades
Check for wear, installation quality, and parallelism.
Fourth: Left/Right cylinder synchronization
Check the levelness of the blade carrier and the consistency of movement between the left and right sides.
Fifth: Frame/Guideways/Worktable
Check for deformation and wear resulting from long-term use.
Addressing these five areas usually resolves a significant portion of shearing precision issues.
 English
 Spanish
 Portuguese
 Russian
 Arabic
 French
 Italian
 German
 Polish
 Thai
 Vietnamese
 Lithuanian
 Czech
 Korean
 Japanese
 Chinese